
Procurement guide
Conveyor, Buffer and Water Bottling Line Integration
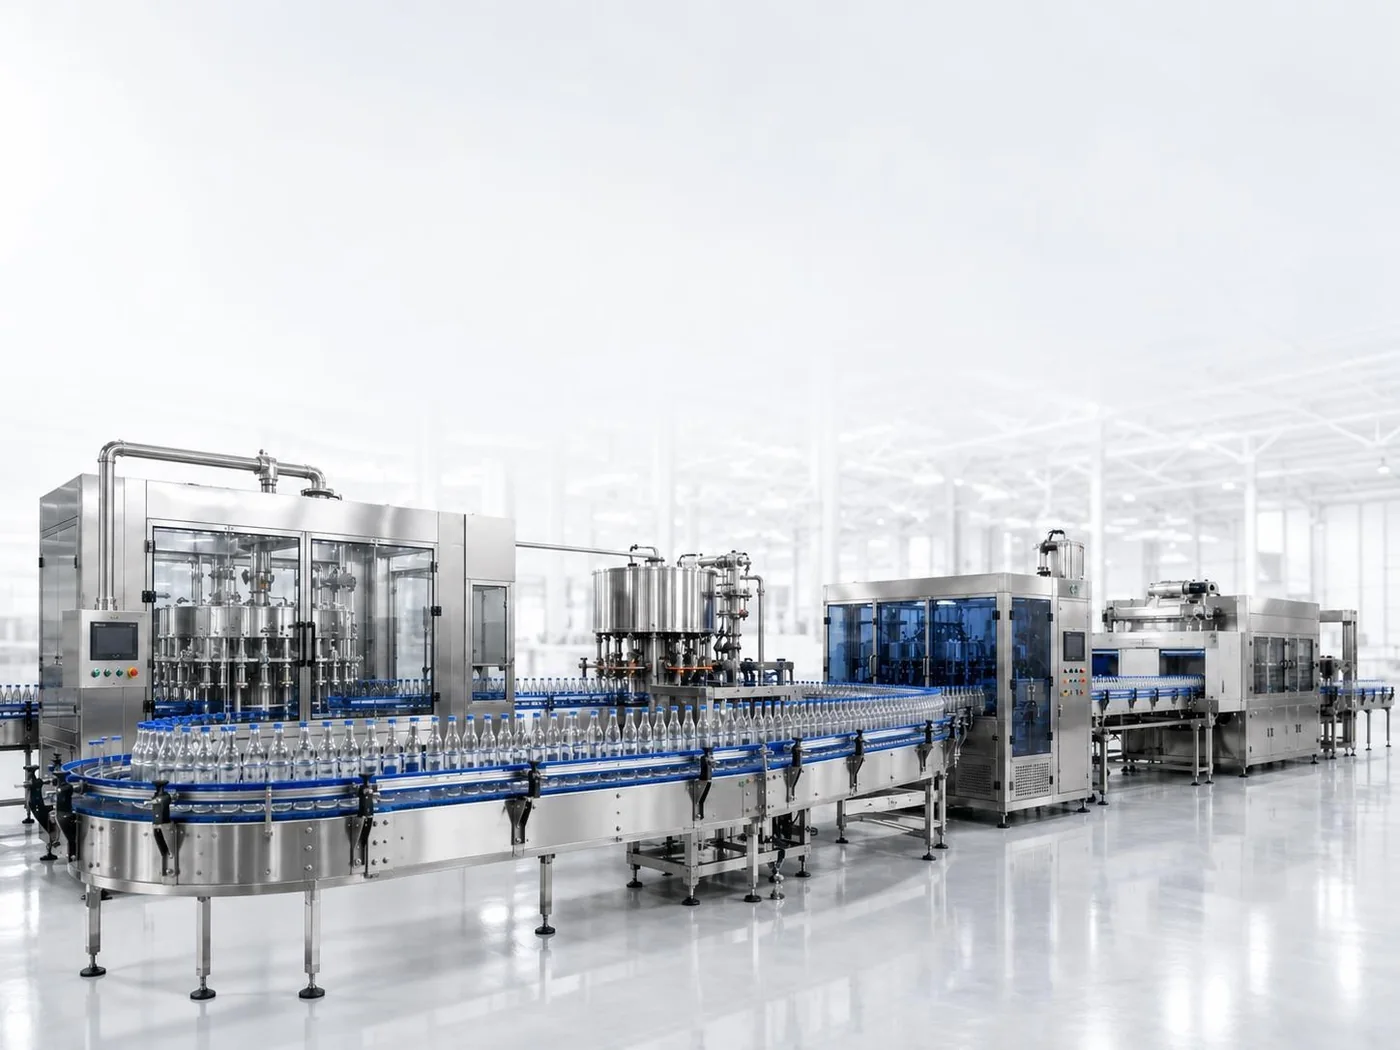
Coordinate transfers, accumulation, elevations, speeds, control signals, guarding and access across equipment supplied by different factories.

Direct answer
Line integration succeeds at the interfaces. Define each transfer condition, acceptable accumulation, stop-and-start logic, responsibility boundary and site measurement before fabrication.
Buyer intent
What this page should help you decide
Evaluate a water bottling machine or line module before requesting a model and price.
Match the equipment function to the real product, container, output, utilities and line interfaces.
A project-specific equipment specification and a list of supplier evidence required for selection.
Procurement workflow
How to move from research to an approved decision
Use the following checkpoints to turn the search for Conveyor, Buffer and Water Bottling Line Integration into a controlled, comparable supplier decision.
Inputs needed for correct selection
A credible selection for Conveyor, Buffer and Water Bottling Line Integration starts with product properties, container drawing, neck and closure data, label and pack format, output at a stated reference volume, operating hours and utility conditions. Confirm Interfaces and Accumulation before discussing a final model.
What a technical offer should show
Require the proposed machine function, rated and expected output basis, contact materials, change parts, control components, utility consumption, footprint, interfaces and supplied documentation. Evidence for Control Signals should match the offered configuration.
Common scope and performance gaps
Check infeed and discharge handling, accumulation, guarding, inspection, rejects, sanitation, coding, downstream packing and controls integration. A nameplate capacity does not prove stable whole-line output for every bottle format.
Decision gate before model approval
Approve the model only after bottle trials or equivalent evidence, line-balance review, layout and maintenance access, acceptance criteria, spare parts and Factory Dimensions are tied to one revision.
What to confirm
Record each item with its source, owner, current status and approval point.
Interfaces
What evidence confirms Interfaces, who owns it, and when must it be approved?
Accumulation
What evidence confirms Accumulation, who owns it, and when must it be approved?
Control Signals
What evidence confirms Control Signals, who owns it, and when must it be approved?
Factory Dimensions
What evidence confirms Factory Dimensions, who owns it, and when must it be approved?
Buyer decision record
| Item | Status | Owner | Evidence |
|---|---|---|---|
| Interfaces | Open | To assign | To request |
| Accumulation | Open | To assign | To request |
| Control Signals | Open | To assign | To request |
| Factory Dimensions | Open | To assign | To request |
Questions to ask the supplier
- What evidence confirms Interfaces, who owns it, and when must it be approved?
- What evidence confirms Accumulation, who owns it, and when must it be approved?
- What evidence confirms Control Signals, who owns it, and when must it be approved?
- What evidence confirms Factory Dimensions, who owns it, and when must it be approved?
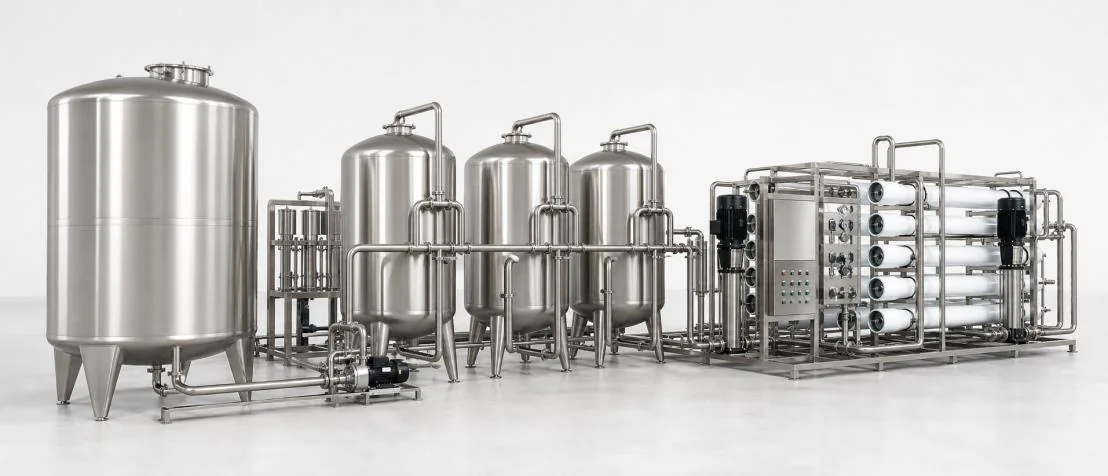
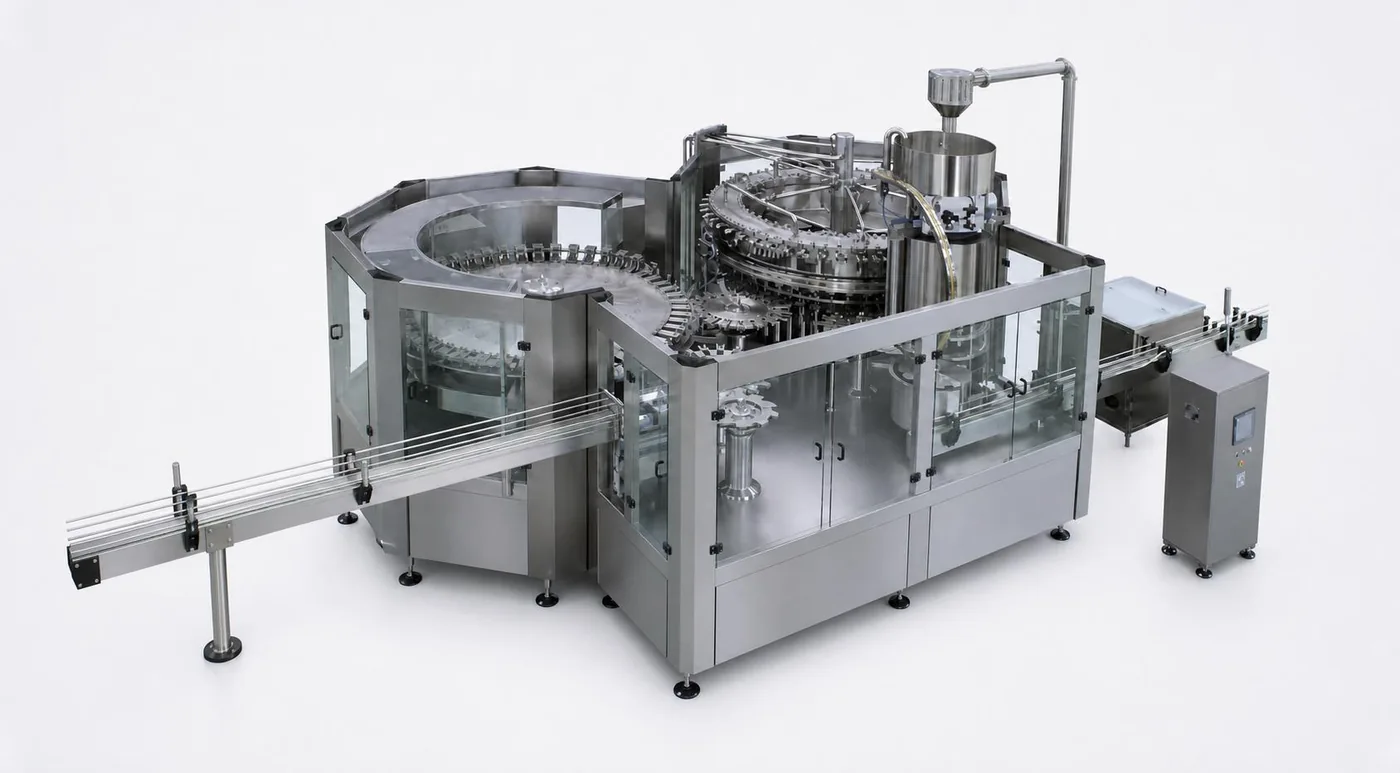
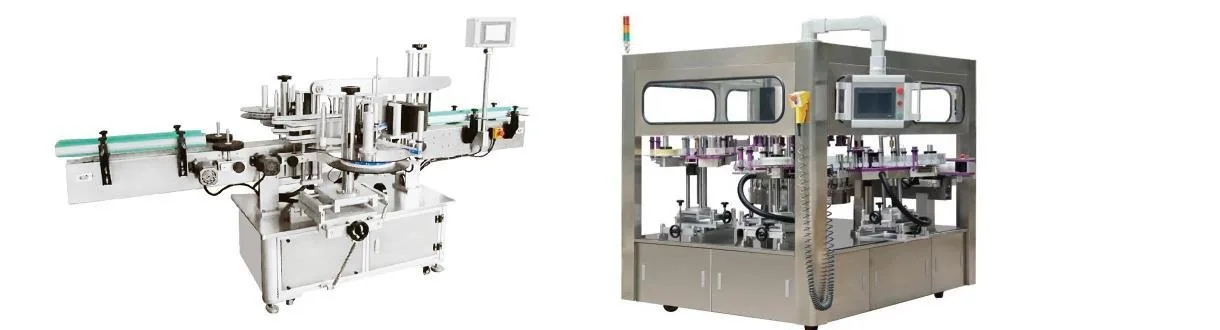
Representative equipment reference. Final models and configuration are project-specific.
2026 catalog reference
End-of-line integration sequence shown
- Labeling and coding precede final pack-out in the reference chain
- Conveying and buffering connect machine functions
- Secondary packing precedes pallet handling
- Controls, accumulation and reject logic remain project-specific
Reference values are not a statement of current availability. Final product range, configuration, output and service scope require project-specific confirmation.
Equipment scope
Representative equipment reference. Final models and configuration are project-specific.
Buyer FAQ
Frequently asked questions about Conveyor, Buffer and Water Bottling Line Integration
What information is needed before requesting a quotation for Conveyor, Buffer and Water Bottling Line Integration?
Start with the finished product, container and closure data, target output with a reference volume, required equipment scope, factory conditions, utilities, destination and schedule. For this topic, confirm Interfaces and identify every unknown rather than allowing an unstated assumption.
How should buyers compare supplier responses for Conveyor, Buffer and Water Bottling Line Integration?
Issue the same revision to each supplier and compare compliance, deviations, inclusions, exclusions, interfaces, evidence, schedule and total commercial exposure. Normalize Accumulation; a headline price or capacity cannot be compared fairly when the underlying scope differs.
What evidence should support a Conveyor, Buffer and Water Bottling Line Integration proposal?
Request evidence that matches the offered configuration, such as drawings, calculations, component schedules, relevant project records, inspection and FAT documents, certificates where applicable, and a written service boundary. Give Control Signals an owner and approval status.
When is a Conveyor, Buffer and Water Bottling Line Integration quotation ready for contract review?
It is ready only when the offered configuration, output basis, utilities, interfaces, documentation, acceptance method and service scope are project-specific and internally consistent. Catalog values remain reference information; resolve Interfaces, Accumulation and Control Signals in the controlled quotation set.
Related buyer guides
Next step